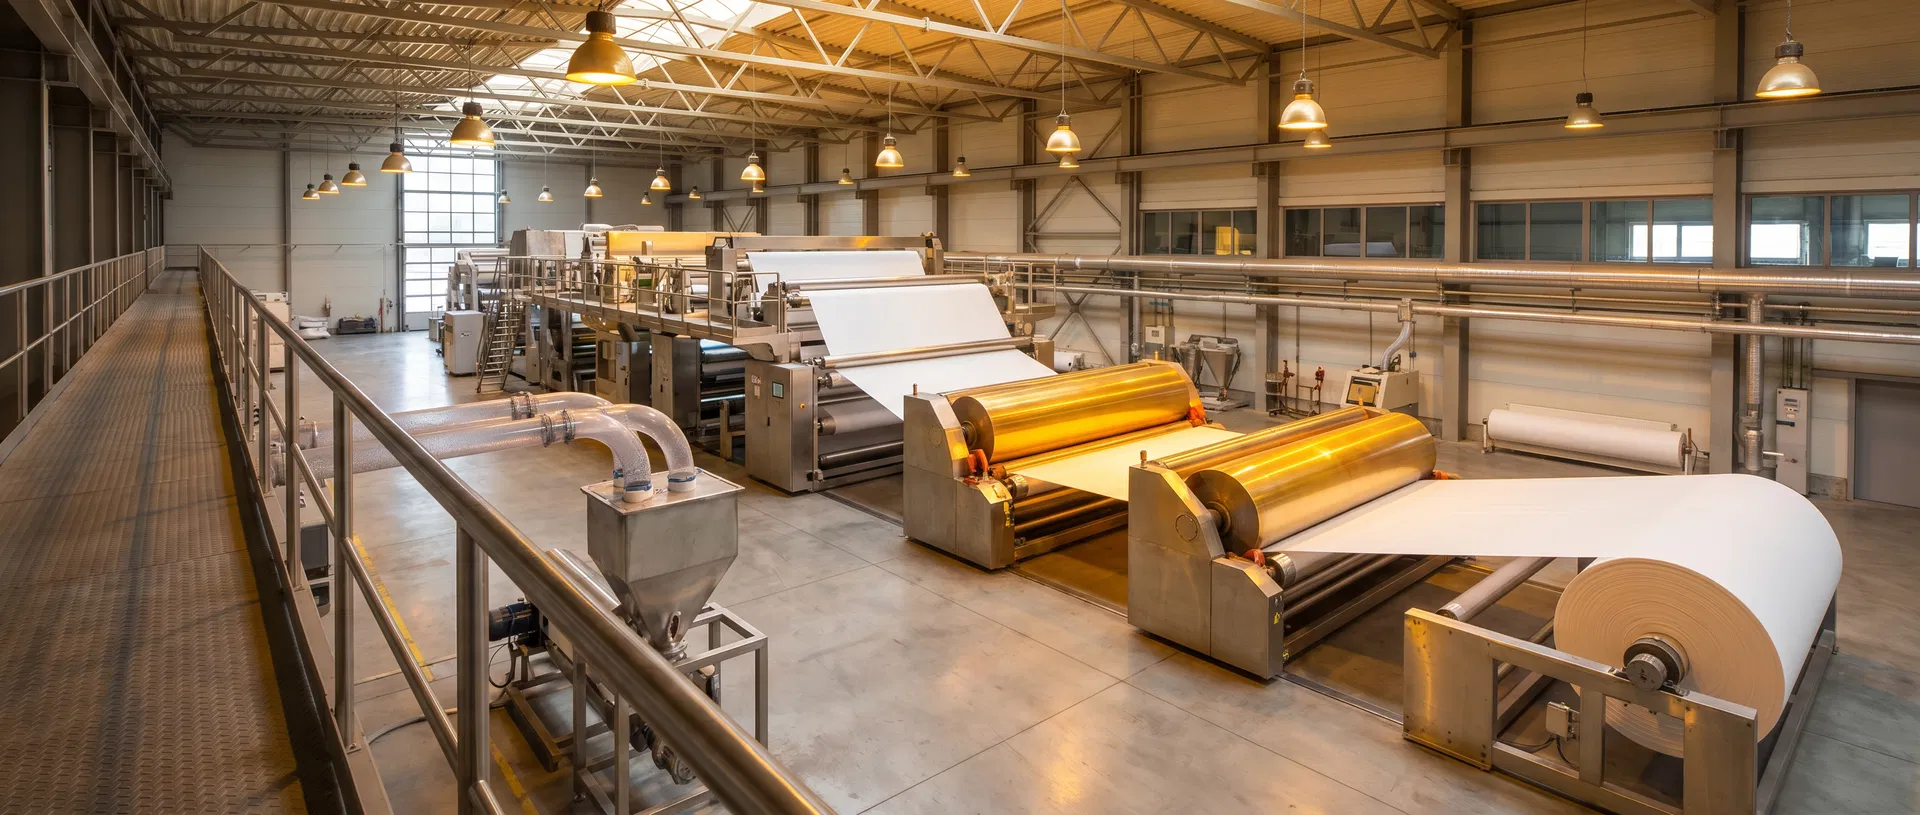
Manufacturing Process
From raw PP granules to finished non-woven products — follow the journey through our state-of-the-art spunbond production facility.
Five Stages of Spunbond Manufacturing
Each stage is precisely controlled and monitored to ensure consistent quality from raw material to finished product.
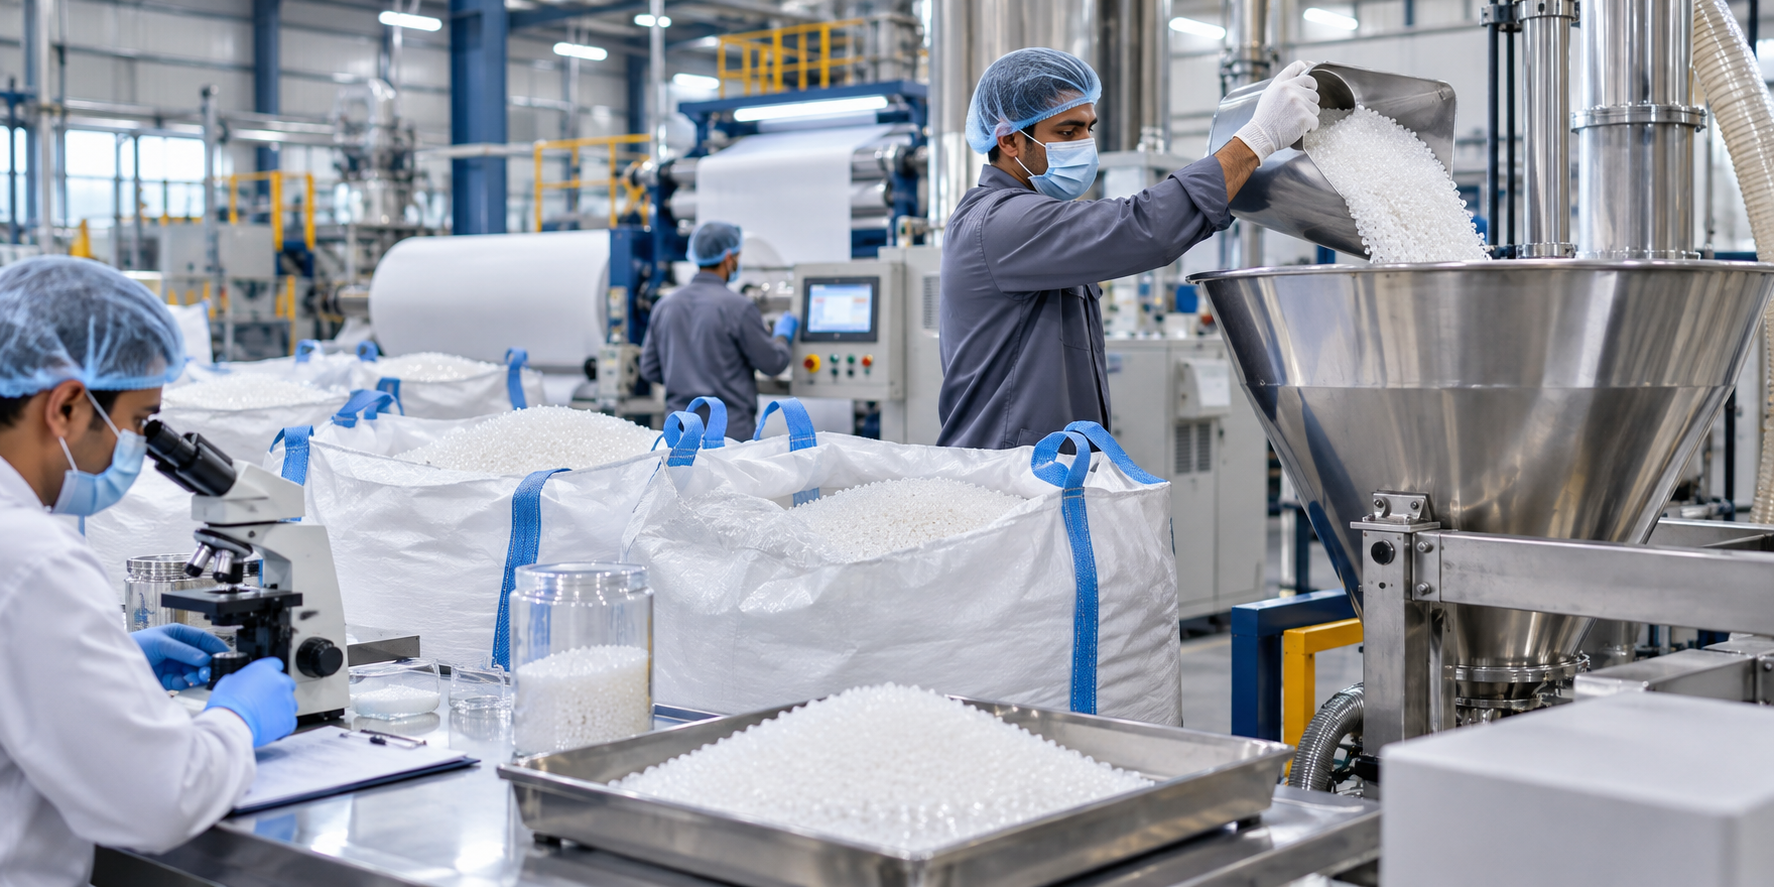
Raw Material Input
Virgin PP Granules
100% virgin polypropylene granules are carefully sourced and quality-tested before entering the production hopper. Each batch is verified for melt flow index, purity, and consistency.
Material: 100% Virgin PP
Melt Flow Index: Controlled
Purity: Laboratory Tested
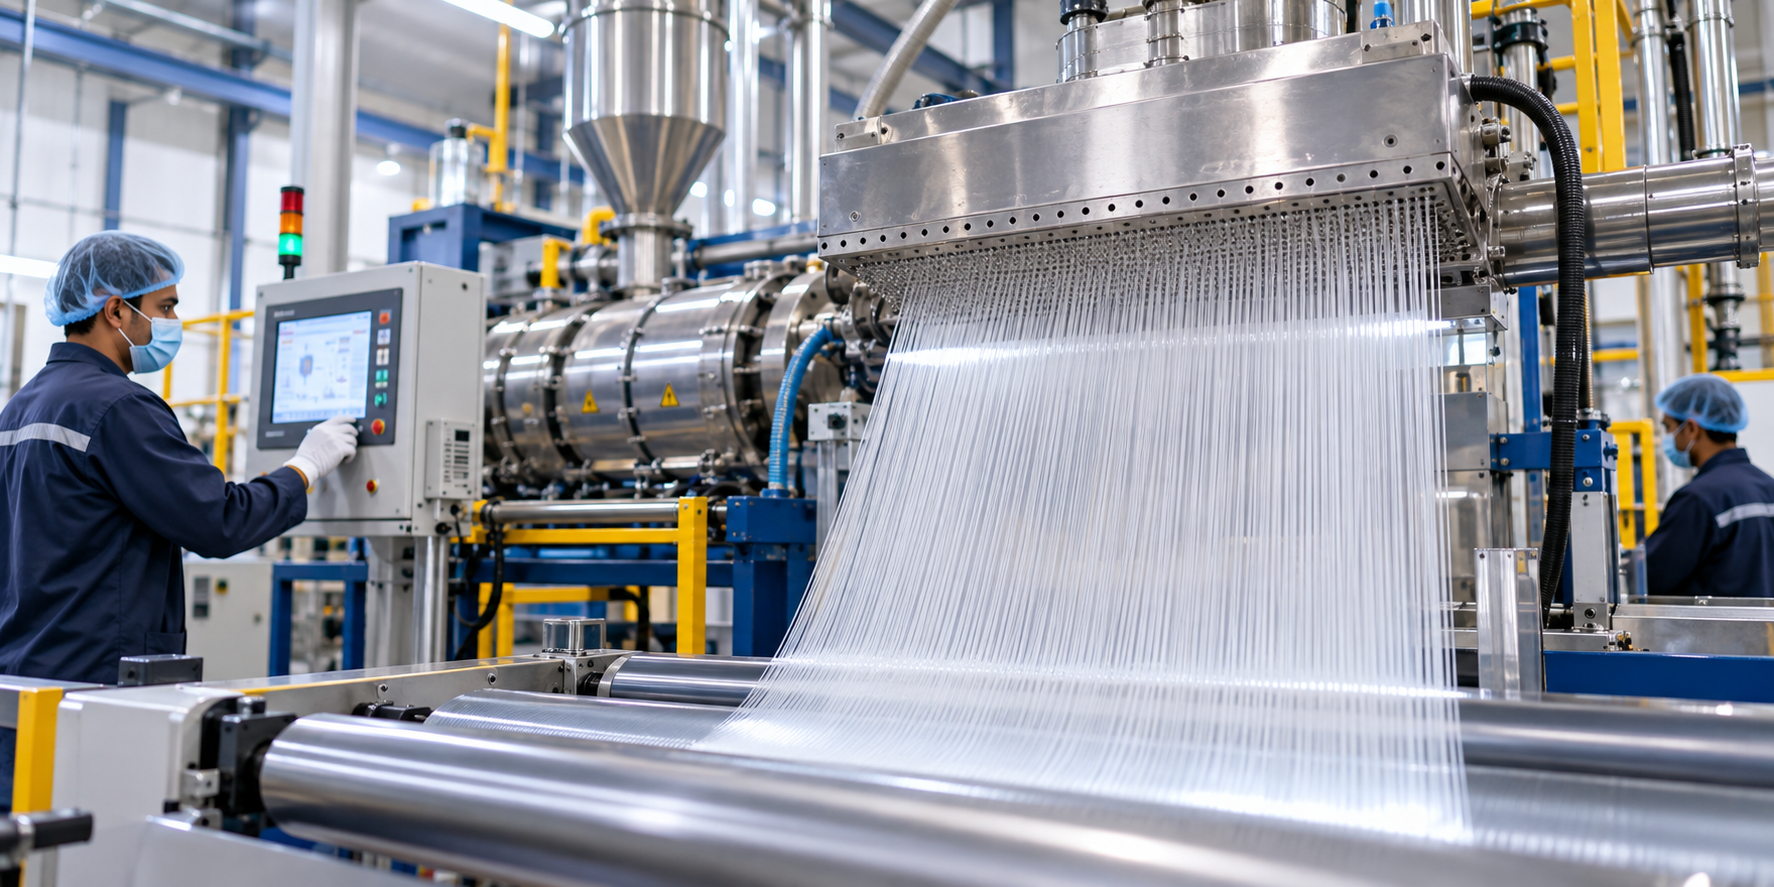
Melt & Extrusion
Spinneret Processing
PP granules are melted at precisely controlled temperatures and extruded through thousands of fine spinnerets to form continuous filaments. Temperature precision ensures uniform fiber diameter.
Temperature: Precisely Controlled
Spinnerets: Thousands of nozzles
Output: Continuous filaments
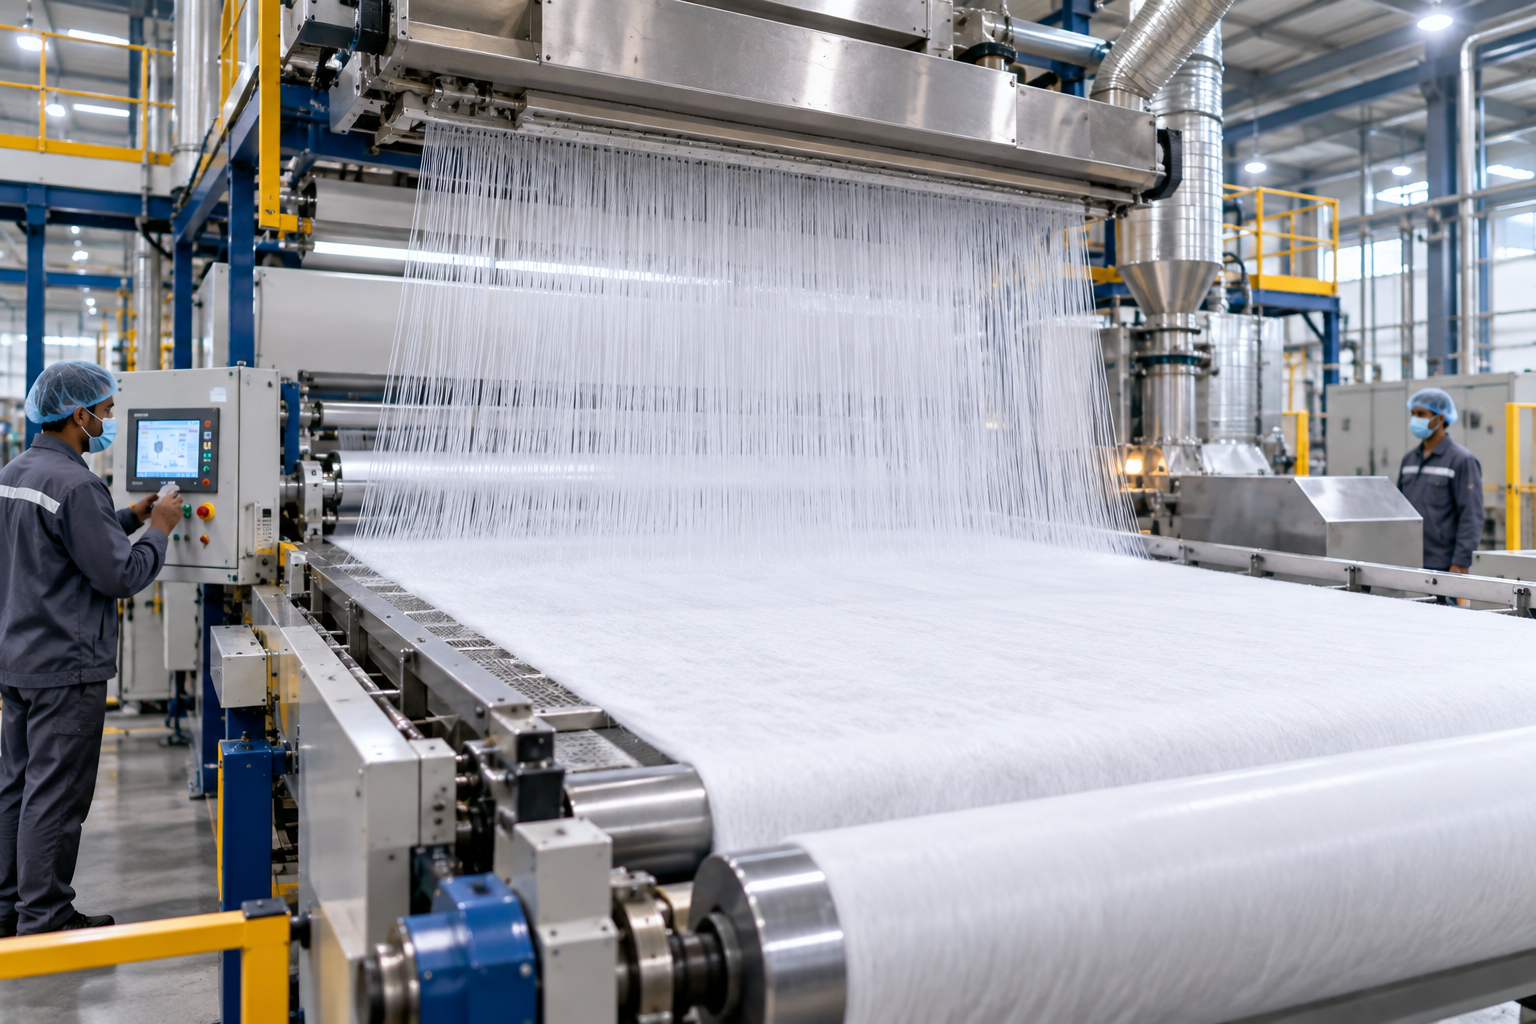
Web Formation
Filament Laydown
Extruded filaments are laid onto a moving conveyor belt in a random pattern to form a uniform web. Air suction from below ensures even distribution and consistent fabric density.
Pattern: Random fiber laydown
Distribution: Air-suction controlled
Width: Up to 3.2 meters
Thermal Bonding
Calender Roll Process
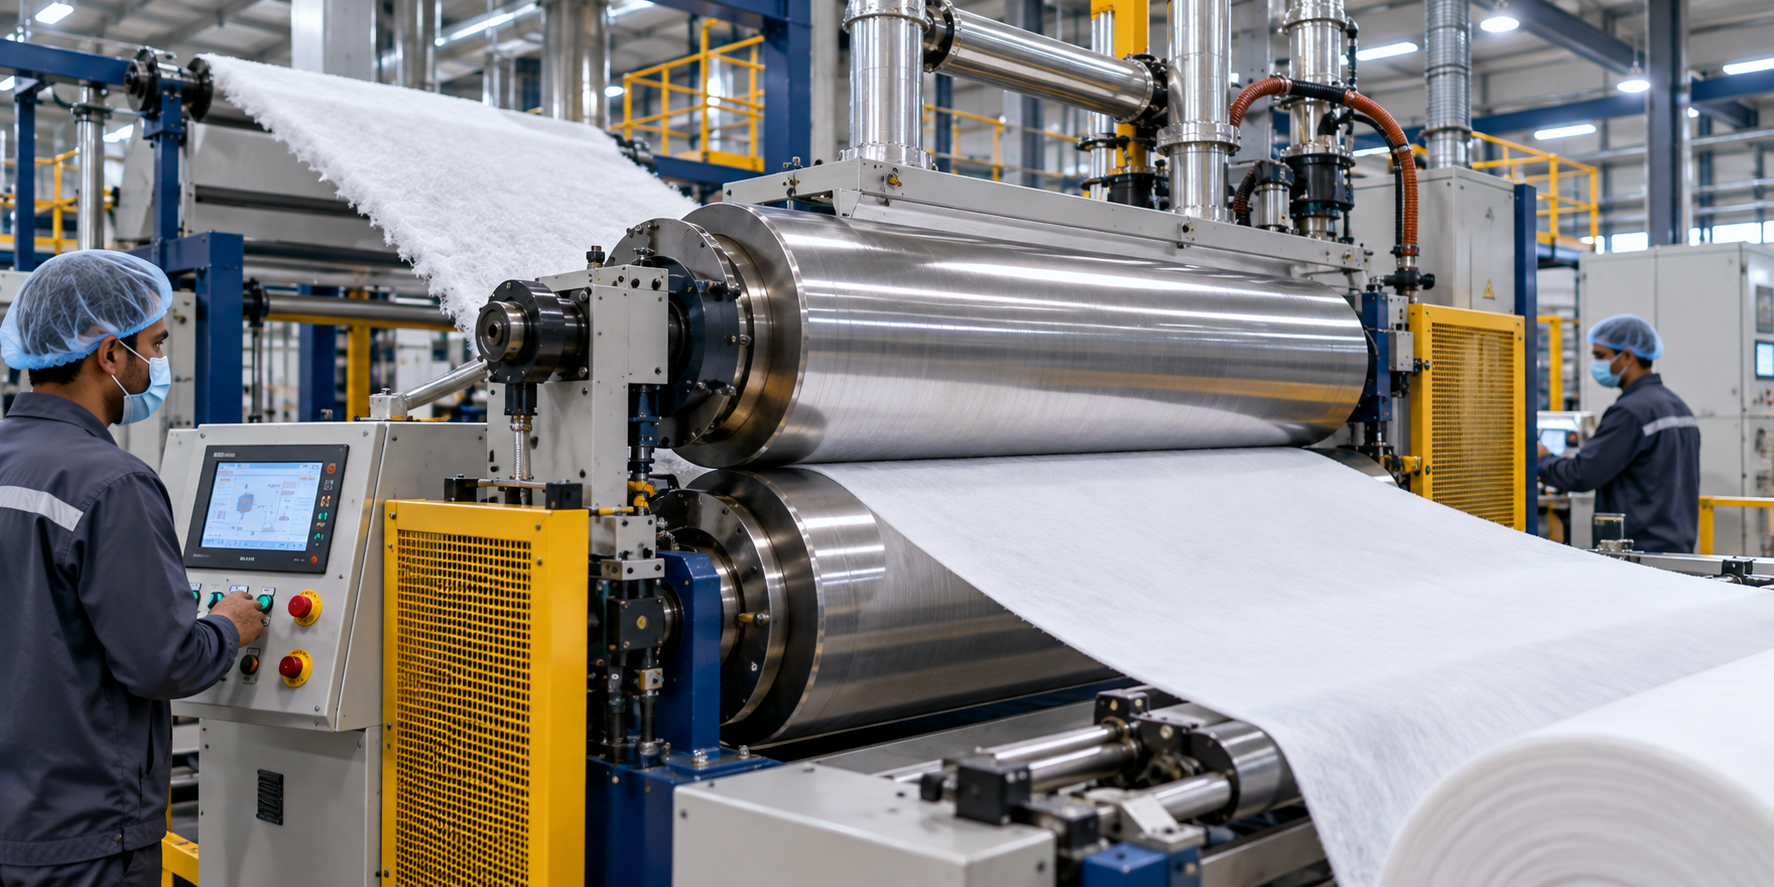
The fiber web passes through heated calender rolls that apply precise temperature and pressure. This thermally bonds the fibers at their crossing points, creating a strong, cohesive fabric.
Method: Thermal calender bonding
Pressure: Precisely calibrated
Result: Strong fiber bonds
Finished Product
Cutting & Conversion
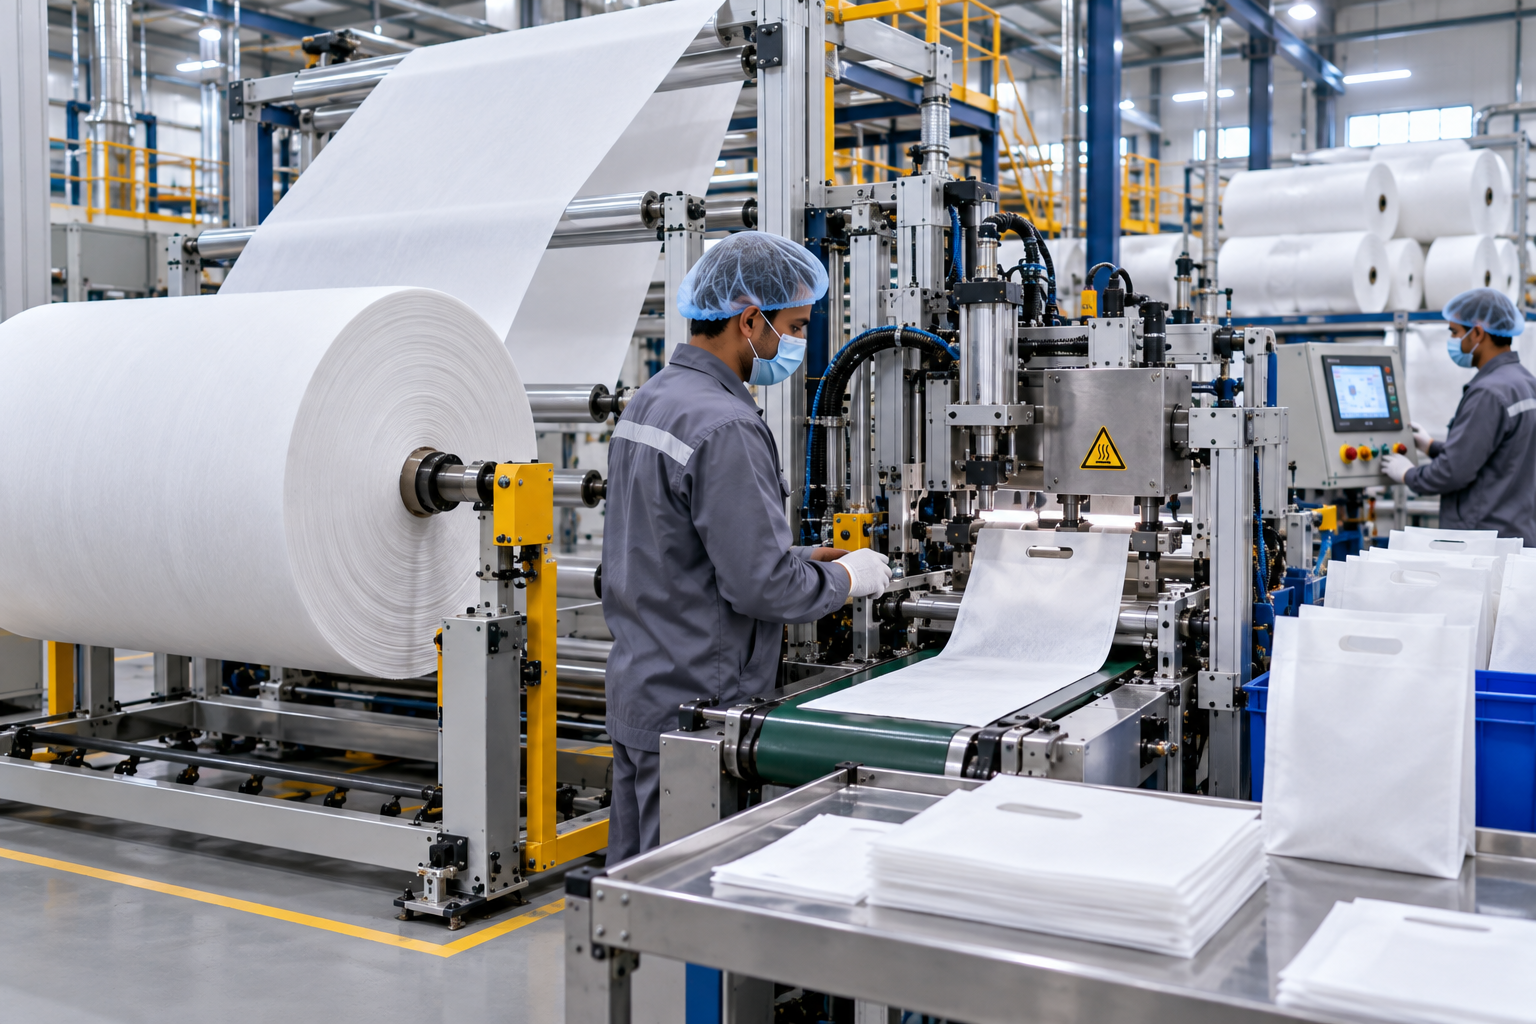
The bonded fabric is wound into rolls or fed directly into bag conversion lines. Ultrasonic sealing machines cut and seal bags without thread or adhesive, producing clean, strong seams.
Output: Rolls or finished bags
Sealing: Ultrasonic technology
GSM Range: 8–150 GSM
Ultrasonic Heat Sealing
Unlike conventional stitching or adhesive bonding, our ultrasonic sealing technology uses high-frequency vibrations to generate localized heat at the fabric interface. This creates a molecular-level bond between fabric layers.
The result is a seam that is stronger than the fabric itself — with no thread, no adhesive, and no weak points. This is a critical differentiator for our finished bag products.
Ultrasonic Vibration
High-frequency molecular bonding
Rigorous Testing at Every Stage
Our in-house ISO-certified quality laboratory ensures every meter of fabric and every finished bag meets exacting standards.
GSM Verification
Every batch tested for weight consistency within ±3% tolerance
Tensile Strength
Machine and cross-direction tensile strength testing per ISO standards
Color Consistency
Spectrophotometer testing ensures batch-to-batch color uniformity
Elongation Testing
Fabric stretch and recovery tested for application suitability
Hydrostatic Pressure
Water resistance testing for medical and laminated fabrics
Bacterial Filtration
BFE testing for anti-bacterial and medical-grade fabrics